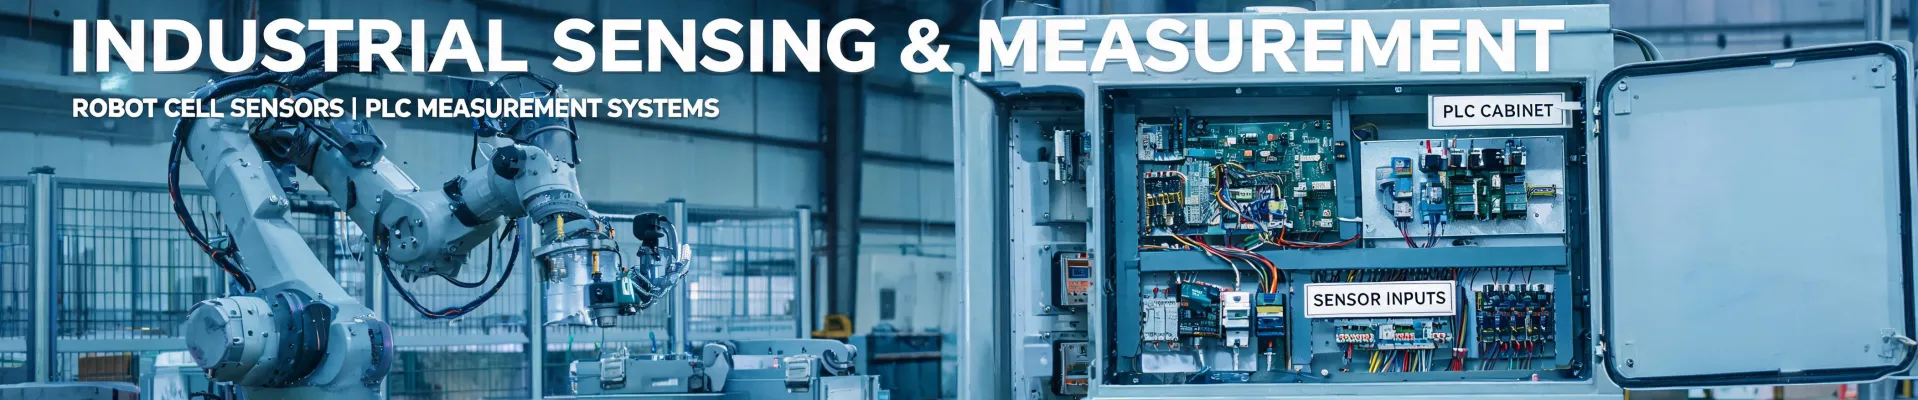
I'm a quality and brand compliance manager at a mid-size contract manufacturer. I review incoming materials and outgoing finished goods on roughly 150 part numbers a year, and I've been doing this long enough to know that inspection choices are rarely about one brand being better than another. They are about matching the tool to the physical signal you need to catch. That's where a Cognex vision system, a laser distance meter, an 83 multimeter, and a thermal camera actually end up in different parts of the toolbox.
Start with the signal, not the brand
When someone asks me about Cognex, they usually expect a camera model recommendation. I usually ask a different question first: what kind of defect are you trying to detect, and how often can you detect it?
A Cognex vision system is excellent at reading codes, checking presence and position, and finding surface defects in visible light. A laser distance meter gives you one dimensional distance with a calibrated number. An 83 multimeter, the one I keep in the maintenance cabinet, measures voltage, current, and resistance. A FLIR thermal camera shows heat patterns before visible failure appears. They are not interchangeable, and pretending otherwise is how quality budgets get wasted.
Three scenarios, three different toolboxes
In practice, I see most inspection projects fall into one of three scenarios. Each points to a different tool.
Scenario 1: In-line inspection on every unit
If you need to inspect every part while the line is running, a human sampling plan is a weak point. I learned this in an avoidable way during a Q1 2024 audit. We had a labeling operation running around 60 units per minute, and an operator was checking the first piece every 30 minutes. A blank label run slipped through for about eight minutes before someone noticed. We reworked roughly 480 units. A Cognex vision sensor would have seen the contrast change immediately and stopped the line.
For this kind of high-speed visual verification, I go straight to machine vision. The Cognex product catalog is the starting point because you can filter by sensor resolution, frame rate, lens mount, and communication protocol. I don't trust my memory on those specs because they change. I use the Cognex login page to get updated datasheets, software compatibility notes, and sample programs before I write an acceptance test.
If you need to read barcodes or DataMatrix codes on every unit, a fixed-mount Cognex reader is usually the answer. If you are checking presence, absence, or assembly details, a vision sensor or an In-Sight camera is often a better fit. But none of those decisions should be made from a product name alone. Use the catalog, get a demo unit, and run your actual parts under your actual lighting.
Scenario 2: First-article and receiving inspection
Not every quality gate runs at line speed. When you are checking incoming parts or evaluating a first article, you have time to set up a measurement and repeat it. In that scenario, a laser distance meter can be enough. If you need to confirm a clearance between a motor bracket and a cabinet door, a laser distance meter gives you a fast numerical answer without building a vision station.
But there is a limit. A laser distance meter measures one point. I once used one to check a door gap across a long seal and missed a bow in the middle because I measured only the two ends. If the feature can vary across a surface, you either scan multiple points or use a vision-based tool that sees the whole geometry. For a simple single-point distance check, though, paying for a machine vision system would be overkill.
Scenario 3: Heat, current, and intermittent failures
Some quality problems don't present themselves in visible light at first. That's where thermal cameras and electrical test tools come in.
If you have ever wondered how does a FLIR thermal camera work, the short explanation is that it uses an infrared sensor array to turn heat into an image. It doesn't read labels, and it won't tell you if a screw is missing. But it will show you a loose electrical connection, an overloaded motor, or a failing bearing before the part stops working. That's why we keep a FLIR camera on a cart for electrical panels and rotating equipment.
For signal troubleshooting, my go-to is still a Fluke 83 multimeter. It lets me verify that a sensor actually has 24 volts, that an analog output is changing, and that a cable shield isn't creating a high resistance path. I've chased what looked like a vision problem for hours, only to find the real cause was electrical noise. The 83 multimeter caught the cause. The camera was just watching the symptom.
How to tell which scenario you are in
When an engineer asks me whether they should buy a Cognex system or something simpler, I walk through three questions:
- Are you inspecting every unit on a live line, or a sample of static parts? Every unit on a live line pushes you toward machine vision. A sample of static parts might be fine with a manual tool.
- Is the earliest defect signal visual, thermal, or electrical? If it's a barcode, orientation, surface defect, or geometry issue, Cognex vision is the right conversation. If it's heat or current, a thermal camera and a multimeter belong in the plan.
- Do you need an image record for traceability? A vision system can archive an image of every unit. A typed number from a laser distance meter is not the same evidence.
That isn't a vague answer. It's a practical decision tree.
One more thing: pricing transparency matters
When you buy any inspection tool, ask what is not included. I've seen quotes that looked low until lenses, lighting, software licenses, and communication modules were added. I've learned to ask about every missing accessory before comparing prices. The supplier who lists everything upfront often looks more expensive on the first page but costs less by the end.
The same logic applies to specifications. A Cognex product catalog is useful only if you use the current version and check the details. The Cognex login page is there for a reason. Download the actual datasheet, verify the interface, and build your acceptance criteria around measurable specs instead of brand trust alone.
At the end of the day, don't ask which tool is best. Ask what you need to truthfully verify. Once you know that, the right answer gets a lot clearer.
Leave a technical question